Home / Case Studies / Manufacturing
Manufacturing · Multi-site
Nestlé Manufacturing Intelligence
IoT sensor networks and real-time analytics giving plant managers end-to-end visibility of production lines.
The challenge
Plant managers needed live production data across several facilities, with energy and waste measured alongside output.
How it works
- SensorsOn production lines.
- Data pipelineReal-time, plant to cloud.
- DashboardsFor plant managers.
- DecisionsAt plant and executive level.
What PLX built
- IoT sensor networks across production sites
- Live production dashboards for plant managers
- Energy and waste tracked alongside output
- Shared figures for plant and executive decisions
Result
Material waste fell by 31% and energy use by 18%, with plant and executive teams working from the same live production figures.
Related work
More case studies.
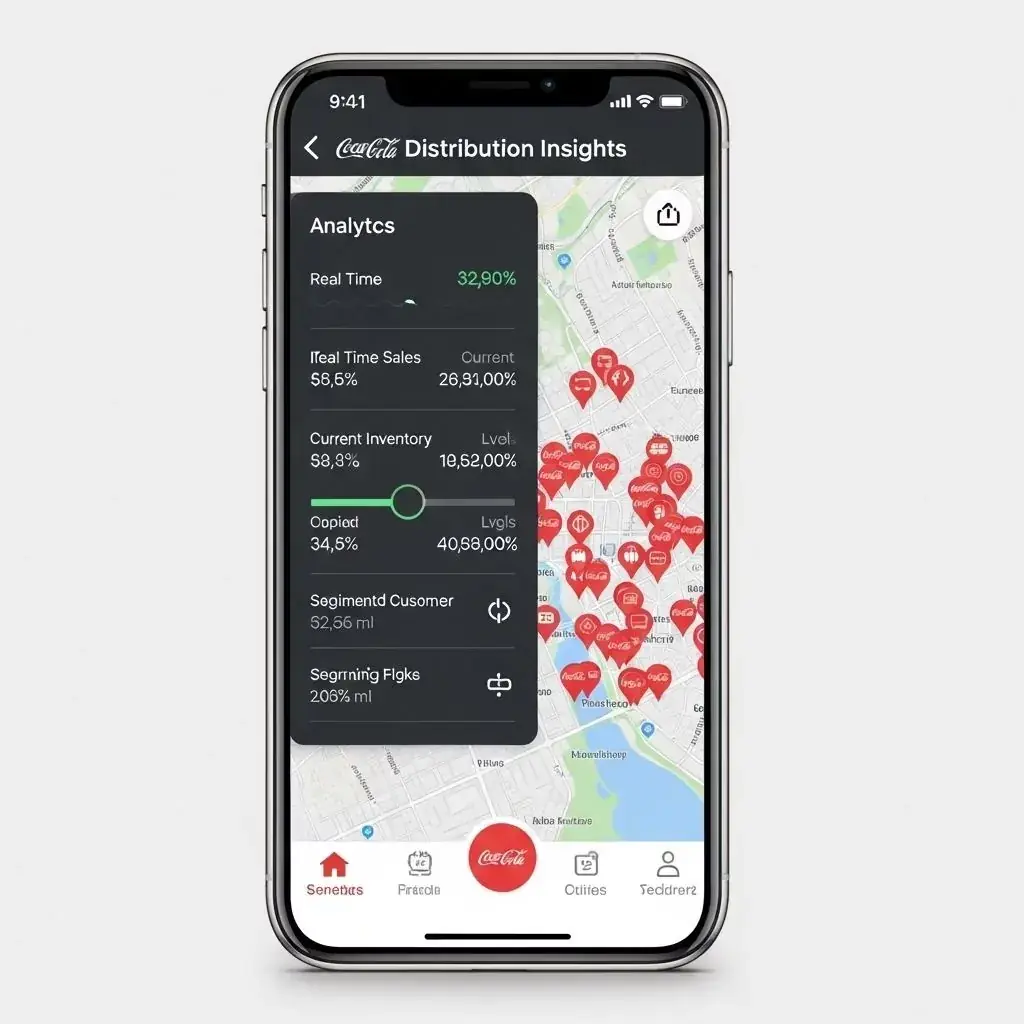
Coca-Cola Distribution App
A sales and distribution app for 2,000 outlets, with offline capability and AI route planning, rolled out in four months.
Read case study →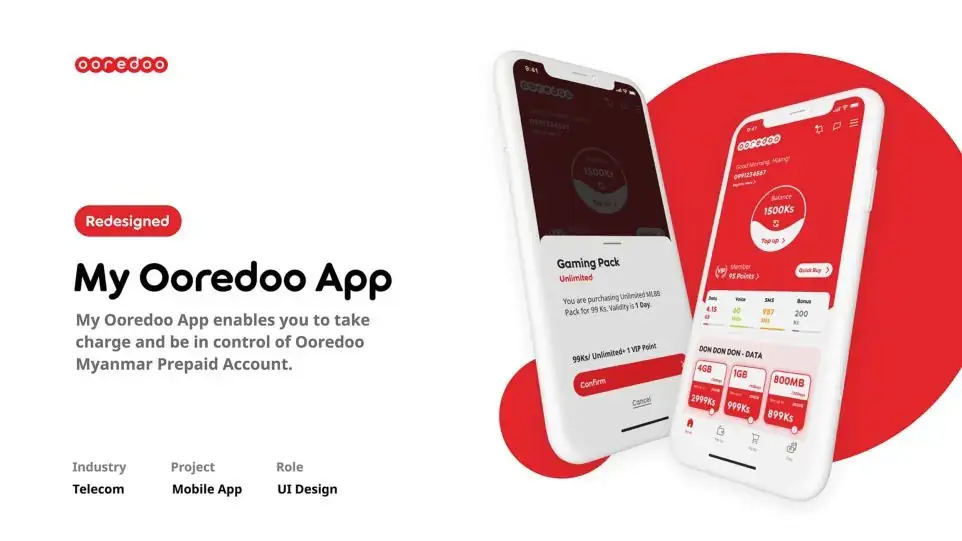
Ooredoo Myanmar Self-Care App
Loyalty, account services, recharges, usage tracking and offers in one app, integrated with legacy billing.
Read case study →
ABG Pocket AI-Assisted Customer Platform
An omni-channel platform that brings web, mobile and social conversations into one interface for support teams.
Read case study →Talk to us about your project.
We reply within 4 hours. Priority requests within 1 hour. Meetings on Zoom, Microsoft Teams or Google Meet.